Waste Activated Carbon Thermal Regeneration System for a Water-Treatment Enterprise
Activated Carbon Production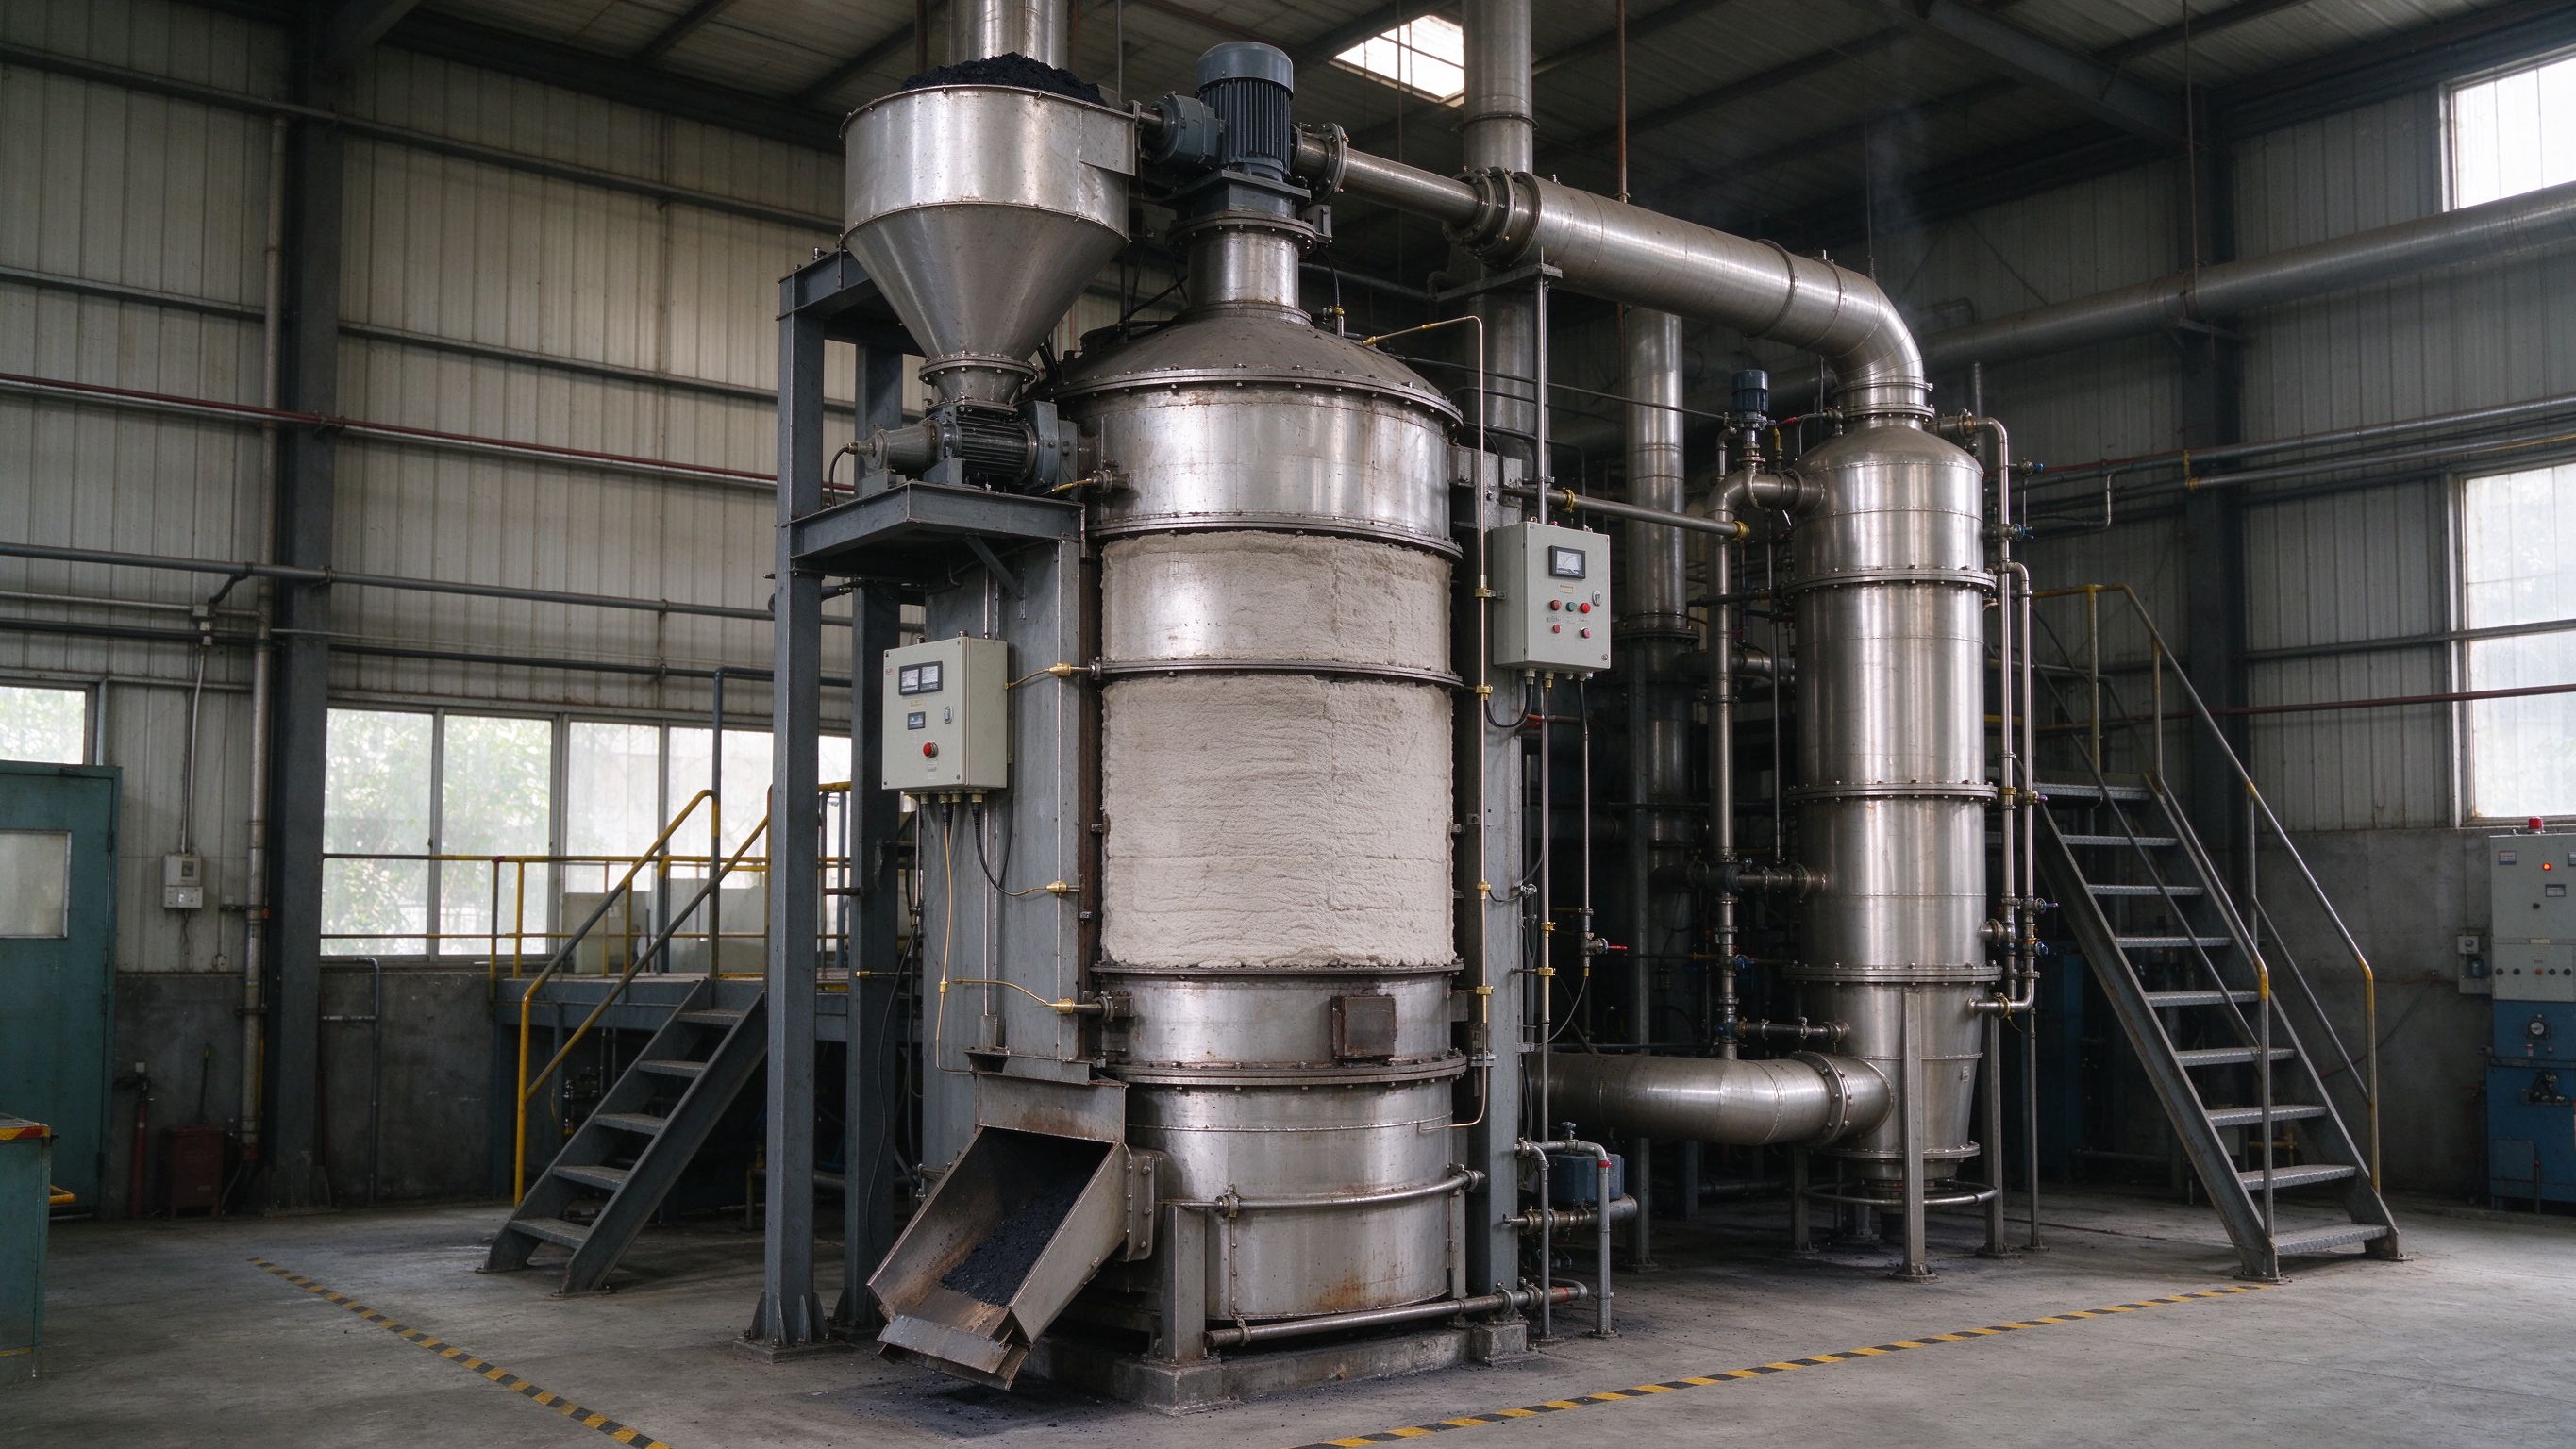
Background
A water-treatment enterprise uses large volumes of activated carbon; replacing saturated carbon is costly and disposal is a burden. The customer wanted on-site thermal regeneration to recover reusable carbon, reduce operating cost, and meet current waste activated carbon thermal regeneration specifications for process and emissions.
Specifications
| Item | Value |
|---|---|
| Regeneration mode | Continuous thermal |
| Regeneration temperature | 700-900 C |
| Iodine recovery | >=85% |
| Regeneration yield | >=90% |
| Off-gas treatment | Incineration + alkali washing |
| Emission standard | Compliant |
Solution
Songrui delivered a continuous activated carbon regeneration furnace with off-gas incineration and alkali washing. Saturated carbon goes through pre-dewatering, drying and regeneration; precise temperature control with oxygen interlock prevents over-burning losses. Regenerated carbon is cooled in a closed system and reused, with automated control and data recording throughout.
Results
| Indicator | Target | Actual |
|---|---|---|
| Iodine recovery | >=85% | 88-92% |
| Regeneration yield | >=90% | 93% |
| Unit energy | - | Notable cost saving vs buying new carbon |
| Off-gas emissions | Compliant | Compliant |
Customer feedback: regenerated carbon meets reuse requirements, procurement and disposal costs dropped significantly.