Low-Ash Wood-Based Activated Carbon Activation Line Revamp, Food Decolorization Client
Activated Carbon Production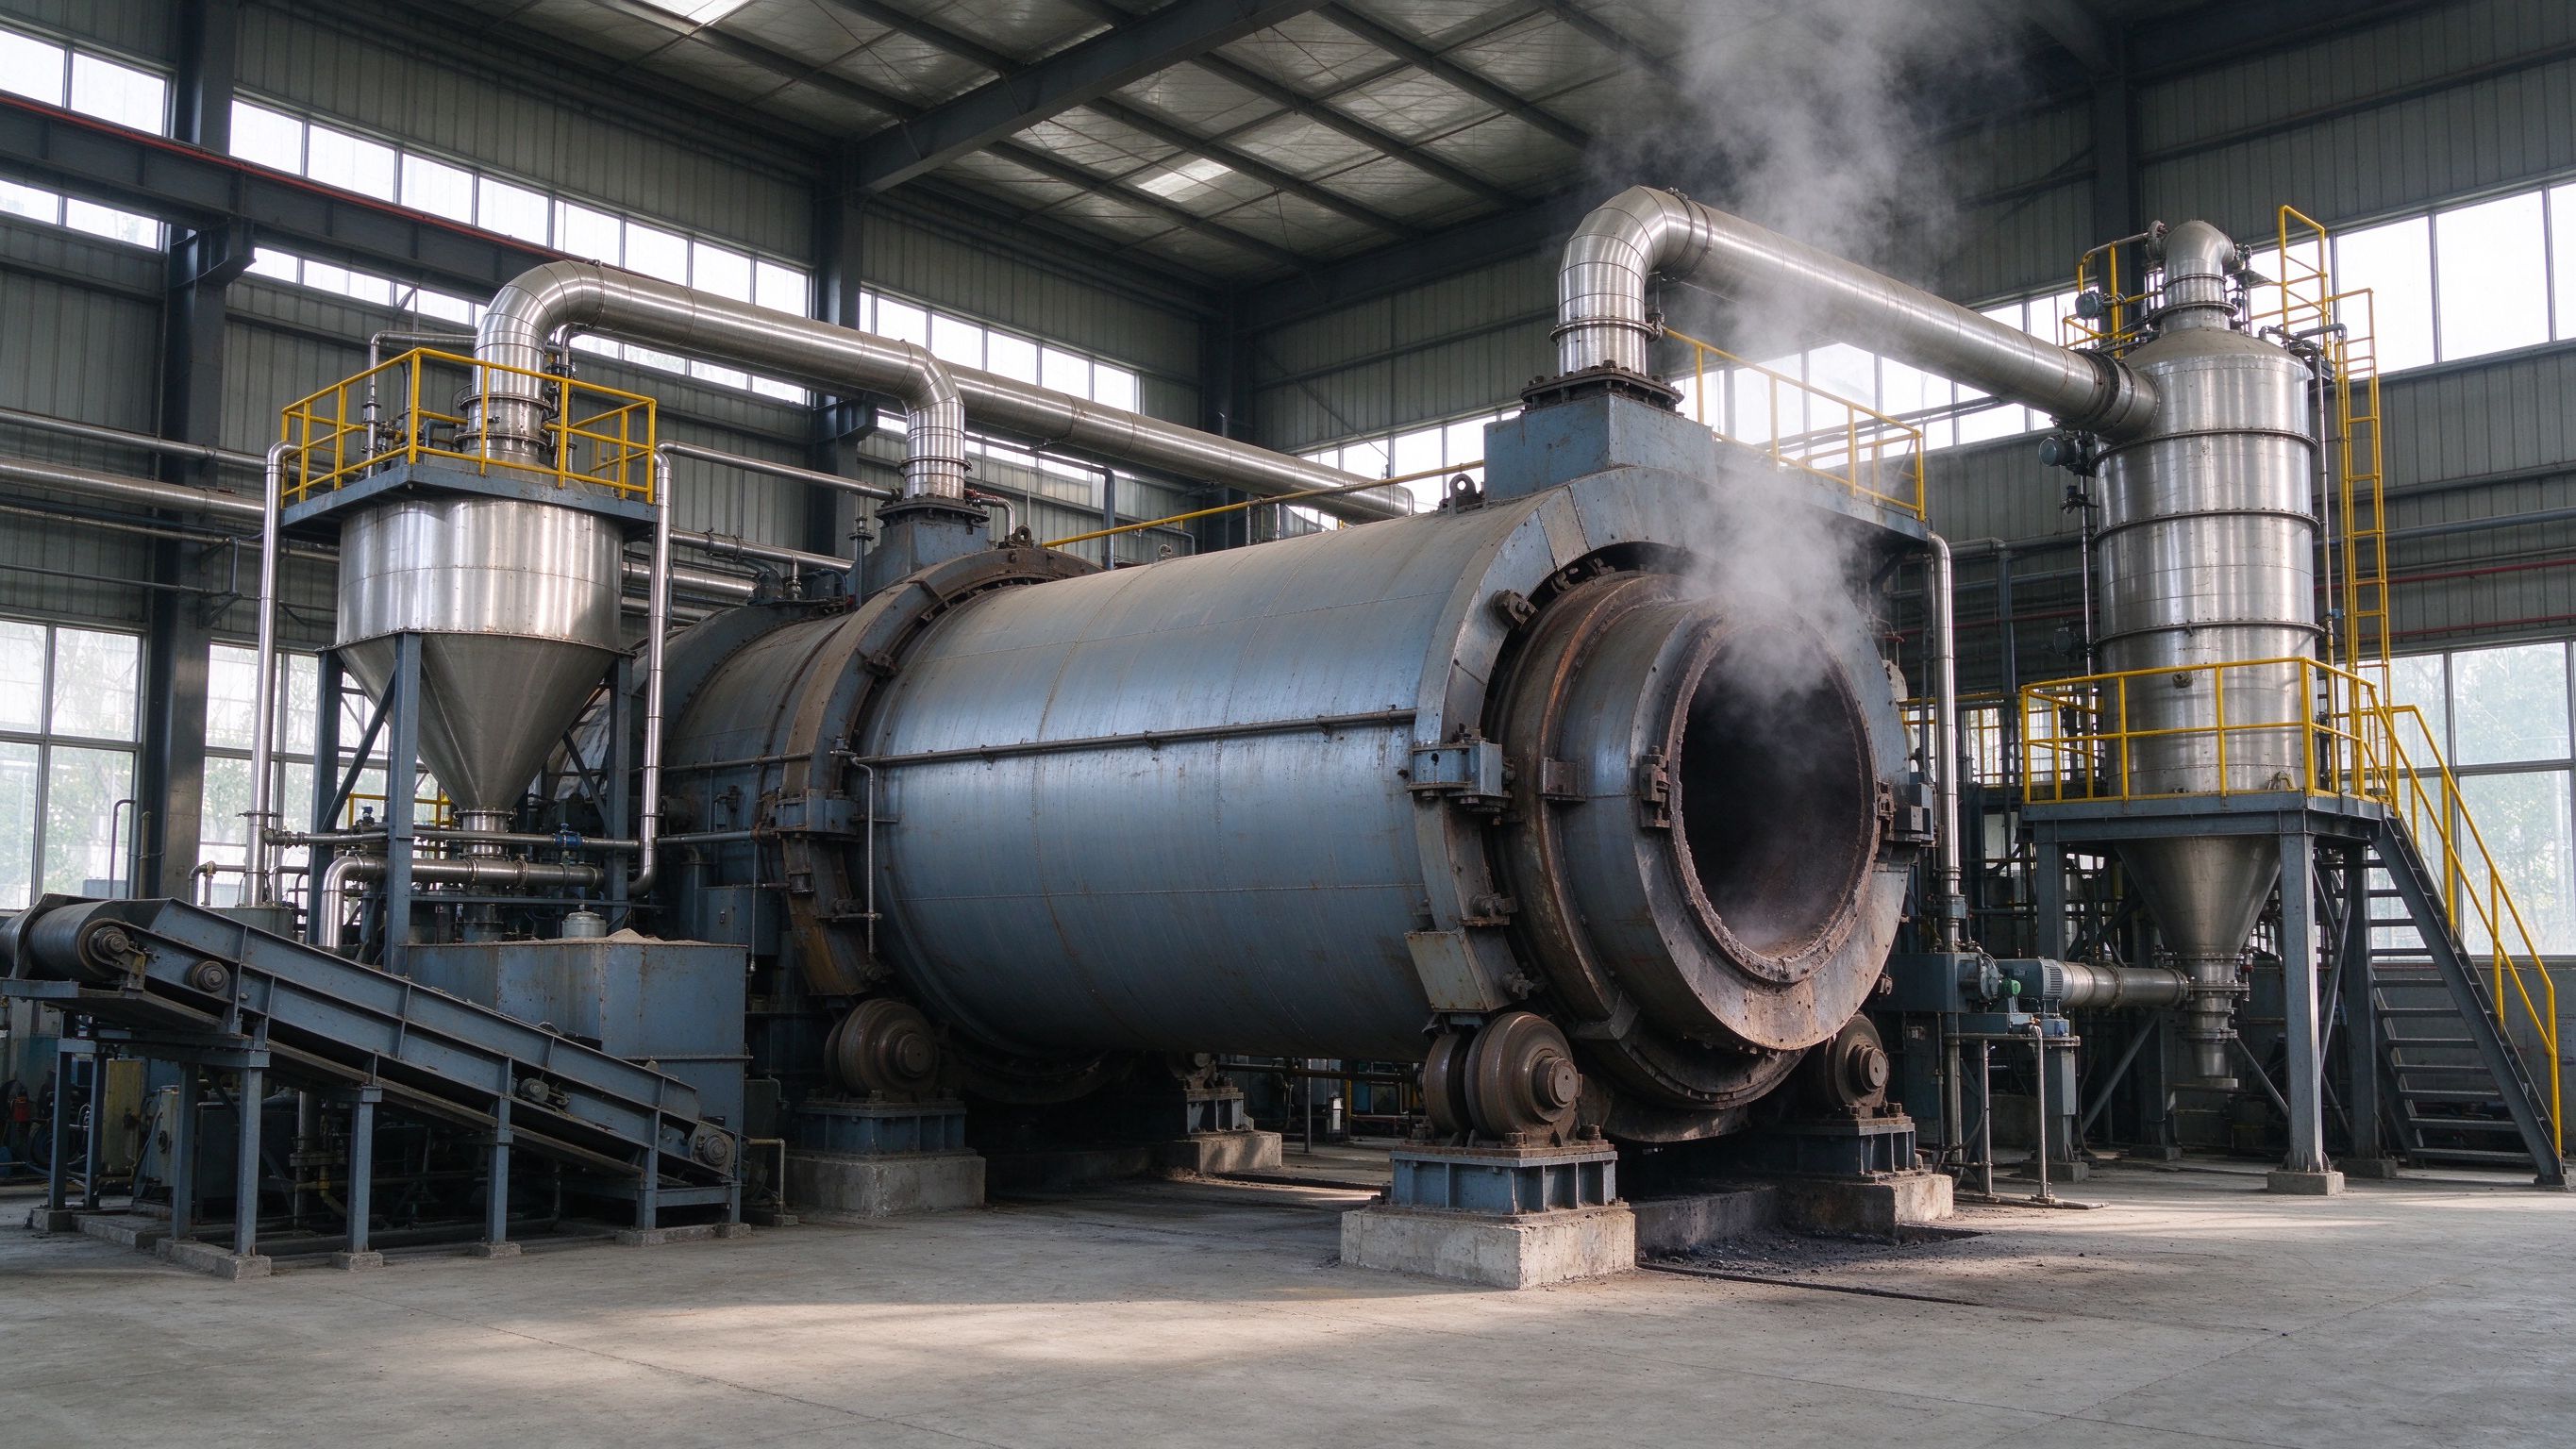
Background
A food and pharmaceutical decolorizing activated carbon producer's existing Slep furnace line aged, with high energy use, fluctuating ash content and batch operation. To meet food-grade low-ash (ash <=3%, high caramel decolorizing rate) requirements, the line was upgraded to 600 t/a continuous activation with off-gas and heat recovery revamp.
Specifications
| Item | Value |
|---|---|
| Capacity | 600 t/a |
| Raw material | Wood-based carbonized material |
| Ash content | <=3% |
| Caramel decolorizing rate | >=90% |
| Main equipment | Continuous rotary activation furnace (replacing Slep furnace) |
| Activation temperature | 850-980 C |
| Refractory | High-alumina castable + insulation |
| Emission control | Off-gas combustion + heat recovery + dedusting |
Solution
After full assessment, the Slep furnace was replaced with a continuous rotary activation furnace, keeping and upgrading feeding, discharging and packaging. Zone temperature control and quantitative steam injection ensure even activation; the shell is cast with high-alumina castable to reduce heat loss, and off-gas heat recovery preheats raw material. For food-grade quality, raw-material cleaning and low-ash testing were added; off-gas combustion and dedusting meet emission limits.
Milestones: old-line assessment and removal (month 1), fabrication and civil revamp (months 2-3), installation (month 4), drying and commissioning (month 5), acceptance (month 6).
Results
| Indicator | Target | Actual |
|---|---|---|
| Capacity | 600 t/a | Achieved |
| Ash content | <=3% | 2.2-2.8% |
| Caramel decolorizing rate | >=90% | 91-94% |
| Unit energy | - | About 18% lower than Slep furnace |
| Continuous operation | Continuous | Stable |
Customer feedback: low-ash stable at food-grade level, continuous process cuts batch turnaround, energy and emission targets met.